Polyurethane Sandwich Panel Production Line Wholesaler: Key Factors for Smart Buyers
2026-08-21
Buying a polyurethane sandwich panel production line isn’t a casual purchase. One wrong spec on heating or foaming pressure can quietly eat your margins for years. Most wholesaler guides stop at price and delivery time—smart buyers dig deeper. This article breaks down what actually separates a reliable line from an expensive lesson, including where YI ZHOU TECHNOLOGY fits into that equation.
Reading Beyond the Spec Sheet: What Actually Determines Output Quality
Numbers on a page rarely tell the whole story. A printer might boast 1200 dpi or a six-color ink system, but those figures don't capture how inks interact with different paper coatings, how gradations hold up in shadow areas, or whether text edges stay crisp under magnification. The real test happens when you compare the same image on matte stock versus glossy, or when a monochrome print reveals slight color casts that spec sheets never mention.
Output quality is shaped by a chain of decisions that start long before the print button is pressed. The source file's color space, the rendering intent chosen in the driver, the age and calibration of the print head, even the ambient humidity in the room—each link affects the final result. A high-resolution file can still produce banding if the printer's screening algorithm struggles with smooth gradients, while a modest 300 dpi image might look stunning when paired with a well-matched ICC profile and paper type.
Perhaps the most overlooked factor is consistency over time. A single perfect print proves little; what matters is whether the tenth print matches the first. Drift in ink density, nozzle clogging, or shifts in paper batch coating can degrade quality silently. Users who measure performance with test charts at regular intervals, rather than relying on initial factory settings, are the ones who end up with output that stays faithful from first page to last.
The Hidden Cost Drivers in Polyurethane Panel Machinery
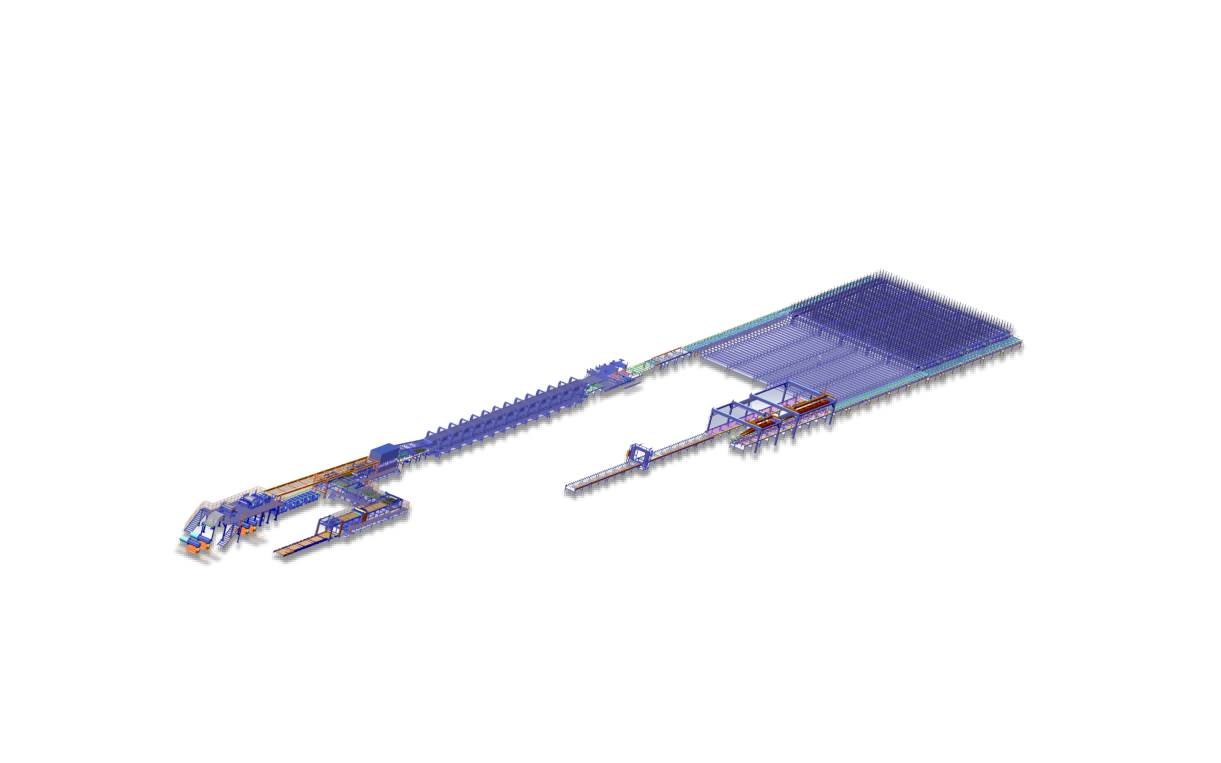
Polyurethane panel machinery often carries price tags that seem straightforward, but the real costs hide in places most buyers overlook at first glance. One of the biggest culprits is the metering system precision. Machines that look similar on paper can differ wildly in how accurately they maintain chemical ratios during high-speed production. Even a small drift in isocyanate to polyol balance leads to foam density variations, which means either wasted raw material or panels that fail insulation tests. Over a year of continuous operation, that inefficiency quietly turns into tens of thousands of dollars in scrap and rework, yet it never appears on the initial invoice.
Another hidden driver sits in the clamping and heating architecture. Cheaper designs often use single-zone platens or uneven pressure distribution, forcing operators to run slower cycle times just to get acceptable panel flatness. The energy draw also shifts: inconsistent temperature control makes the line consume more power per square meter of panel than the spec sheet suggests. Maintenance crews then face frequent belt replacements and hydraulic seal failures because thermal stress concentrates in the same spots repeatedly. These recurring repairs and production slowdowns rarely get factored into the purchase decision, but they dominate the total cost of ownership.
Finally, the automation layer adds cost in less obvious ways. A machine with limited recipe storage or manual changeover procedures might look cheaper upfront, yet every product switch becomes a labor-intensive event. Operators spend hours adjusting pour patterns, trimming speeds, and curing oven settings instead of monitoring quality. Skilled labor is not cheap, and depending on manual tweaks introduces variability that leads to off-spec batches. Machines that memorize and automatically recall validated production parameters reduce that hidden labor burden, but buyers often ignore this until they compare shift logs and realize how much time disappears in setup rather than actual panel output.
Questions Wholesalers Rarely Ask (But Should)
Most wholesalers track margins, turns, and fill rates, but they rarely ask which of their customers actually make the business worse. A quick look at order frequency, return rates, and the time spent on special requests can reveal that a handful of accounts are eroding profit. Dropping or repricing them often feels uncomfortable, yet it is usually more valuable than chasing another low-margin deal. That is a question worth asking before the next sales meeting.
Another absent question is what would happen if the top supplier or top customer disappeared overnight. Many wholesalers have no written answer, no backup sourcing plan, and no idea which relationships are truly loyal versus merely convenient. Running a simple key person risk exercise for both supply and demand sides exposes gaps that a balance sheet will not show.
Wholesalers also shy away from asking how their own buying habits shape customer behavior. If every negotiation focuses on price, customers learn to treat the product as a commodity. Asking what value is being added beyond the box itself, such as repacking, forecasting help, or reliable delivery windows, can shift the conversation away from constant margin pressure. Few distributors pause long enough to see that the questions they avoid are often the ones that determine whether they stay relevant.
Matching Line Configuration to Your Real Production Mix
The hardest part of line configuration is admitting your product mix isn't static. Real customer demand shifts from month to month, and a line set up for a single high-volume SKU will bleed time and money when you have to run ten smaller ones. Before touching equipment, pull the last twelve months of actual orders—not the forecast—and group them by routings. You'll often find that the mix you planned for represents only a fraction of real weekly output.
Once you see the true mix, split it into two or three families based on changeover complexity and order frequency. Put your stable, high-volume products on a dedicated line where takt time is predictable. For the messy long tail, create a flexible zone with movable carts, quick-release fixtures, and operators who can rotate between stations. Trying to make one line serve both extremes usually results in neither running well.
Finally, match buffers and staffing to the actual sequence of work. If your mix includes many small batches, a U-shaped cell with shared tasks beats a long linear conveyor because operators can step into bottlenecks. Track changeover duration per product family and compare it to available shift time. The bottleneck rarely disappears by adding another machine; more often, reconfiguring station positions and rebalancing operator assignments clears the real constraint.
Automation Levels That Pay Back Fastest
Start with the boring, repetitive work. Lower automation levels—like auto-sorting incoming emails, copying data between two systems, or sending a standard follow-up—require almost no setup time, so the payback shows up within weeks. The return isn't dramatic on day one, but ten minutes saved per employee per day adds up before the quarter ends.
One step up, process-level automation that still includes a human checkpoint tends to clear its cost quickly in areas like billing disputes or inventory updates. The key is to set a narrow trigger and a clear owner. If the software flags an exception and routes it to the right person instead of trying to solve it alone, you avoid the expensive edge cases that slow down adoption and kill the return.
High-level autonomy sounds impressive, but it only pays back fast when you already run thousands of identical transactions a day. For everyone else, the fastest payback comes from layering two or three small automations, proving the time savings, then reinvesting that freed-up capacity into the next level. That keeps the investment low and the momentum high.
After the Sale: Service Commitments Worth Getting in Writing
A handshake and a smile might feel reassuring in the moment, but once the paperwork is signed and the keys change hands, memory has a way of bending. The service promises that matter most—response windows, loaner car policies, coverage for wear-and-tear items—rarely hold up in court or in a service bay unless they're spelled out on paper. Before you drive off the lot, ask the dealer to itemize exactly what post-sale support looks like: who answers the phone when a warning light flashes at 9 p.m., how quickly they commit to diagnosing a leak, and whether that "free first inspection" covers parts or just the labor of looking.
Smart buyers treat verbal assurances as placeholders, not guarantees. If a salesperson tells you that software updates are complimentary for the first three years or that a mobile technician will come to your driveway, get it in the buyer's order or a signed addendum. Pay special attention to exclusions buried in the fine print: a warranty that covers the transmission but not the valve body, or a roadside assistance plan that limits towing to fifteen miles. These details determine whether a service commitment is a genuine safety net or a convenient way to deflect responsibility after the sale.
Equally important is knowing who stands behind the promise. A regional distributor might offer extended coverage that the local dealership quietly disavows once a claim is filed. Ask for the name and direct line of the service manager, and confirm whether the commitment transfers if you sell the vehicle before the coverage expires. Written commitments shouldn't read like a legal maze—they should clarify escalation paths, define reasonable turnaround times, and name the person accountable when things go sideways. The goal isn't to anticipate every failure; it's to ensure that when the unexpected happens, the promise isn't just a memory of a friendly conversation.
FAQ
Look beyond the glossy brochure and ask for at least three client references where the line has been running for more than two years. Visit one of those sites if possible, or request a video walkthrough with the actual operator, not a sales rep. Pay attention to how the wholesaler handles questions about line changeover times and whether they can supply a detailed component list before you sign anything.
Request a production log from an existing customer, not just a spec sheet. The line's rated speed means little if it constantly slows down for foam adhesion issues or panel thickness changes. Ask for the average daily output over a month, including shift changes and minor stops. A trustworthy wholesaler will also let you run your own material samples on a test line before purchase.
The mixing head and the double belt conveyor are the usual culprits. Smart buyers insist on quick-release mixing heads that can be swapped without recalibrating the whole line, and they check whether the conveyor's heating plates are individually replaceable. They also ask about the availability of spare parts locally, because waiting three weeks for a custom part from overseas kills production.
For most buyers, a turnkey line from one responsible wholesaler reduces integration headaches, but that only works if the wholesaler actually builds the control system in-house. If they just resell a mix of third-party units, you may end up paying a markup for a line nobody fully understands. Ask who wrote the PLC program and who you call when the alarm goes off at 2 a.m.
Polyol and isocyanate batches vary, especially if you buy from different suppliers. A line that cannot automatically adjust the mix ratio will produce weak spots or uneven density. The wholesaler should provide a detailed calibration procedure and ideally a closed-loop control that monitors pressure and temperature at the mixing head. Ask for trial runs with your actual raw materials, not just reference chemicals.
Remote diagnostic access is a big one. Many buyers only realize they need it when a minor sensor fault shuts down the line and the wholesaler's technician can't fly in for two weeks. Also check whether software updates are included or billed separately, and whether the warranty covers wear parts like seals and mixing nozzles or only major structural failures.
Don't rely on the installed motor power alone. Ask for a specific energy consumption figure per square meter of panel produced at a standard thickness, such as 50 mm. Heating the double belt often accounts for more energy than the drives, so compare how each line recovers heat or insulates the heating zones. A slightly higher upfront price can pay for itself within two years through lower electricity bills.
Foundation work, ventilation upgrades, and compressed air capacity are frequently left out. You may also need a dedicated transformer if the line's total load exceeds your current supply. Then there is training: a good wholesaler includes operator and maintenance training, but travel and accommodation for their trainers is often extra. Always request a line-item quote that separates equipment, installation, commissioning, and training.
Conclusion
Smart buyers look past glossy spec sheets because what truly shapes output quality is how well the line controls foam density, temperature, and mixing pressure under real production conditions—not just the nominal line speed. Many hidden costs come from energy consumption, adhesive overspray, and frequent wear on cutting blades and rollers, which often surface only after months of operation. It pays to ask questions wholesalers rarely raise—who actually manufactures the metering pumps and PLC, what happens to thickness tolerance when you switch facings mid-run, and how much scrap is generated during start-up and shutdown. The answers reveal whether a machine is built for consistent panels or just for a demo.
Matching configuration to your real production mix means being honest about your common panel thicknesses, facing materials, and order sizes. A line with quick-change thickness adjustment and flexible stacking options will outperform a faster line that forces you to stop for manual recalibration. Automation that pays back fastest tends to be in glue spreading, cutting, and automatic stacking—areas where labor costs and material waste are highest. Finally, get service commitments in writing, including guaranteed response time, spare parts availability for critical components, remote diagnostic support, and operator training. Wholesalers who treat after-sale support as part of the product, not a favor, are the ones who keep your line running when demand peaks.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/