Detergent Pods Wholesaler Tips for Buying in Bulk Without Sacrificing Quality
2026-11-21
Buying detergent pods in bulk can feel like a gamble—especially when cheaper options start leaving residue on clothes or fading colors faster than expected. If you're sourcing for a retail shelf, cleaning service, or busy household, the real challenge isn't just finding a low unit price. It's knowing which wholesale suppliers maintain strict quality standards under pressure. That's where a focused approach saves you from costly trial runs and customer complaints. LANJIEYA has built its reputation around consistent pod integrity, measured dissolving times, and packaging that holds up in storage. Before you commit to a large order, a few insider checks can help you separate dependable bulk deals from watered-down formulas.
Where bulk detergent pod quality slips before the first wash
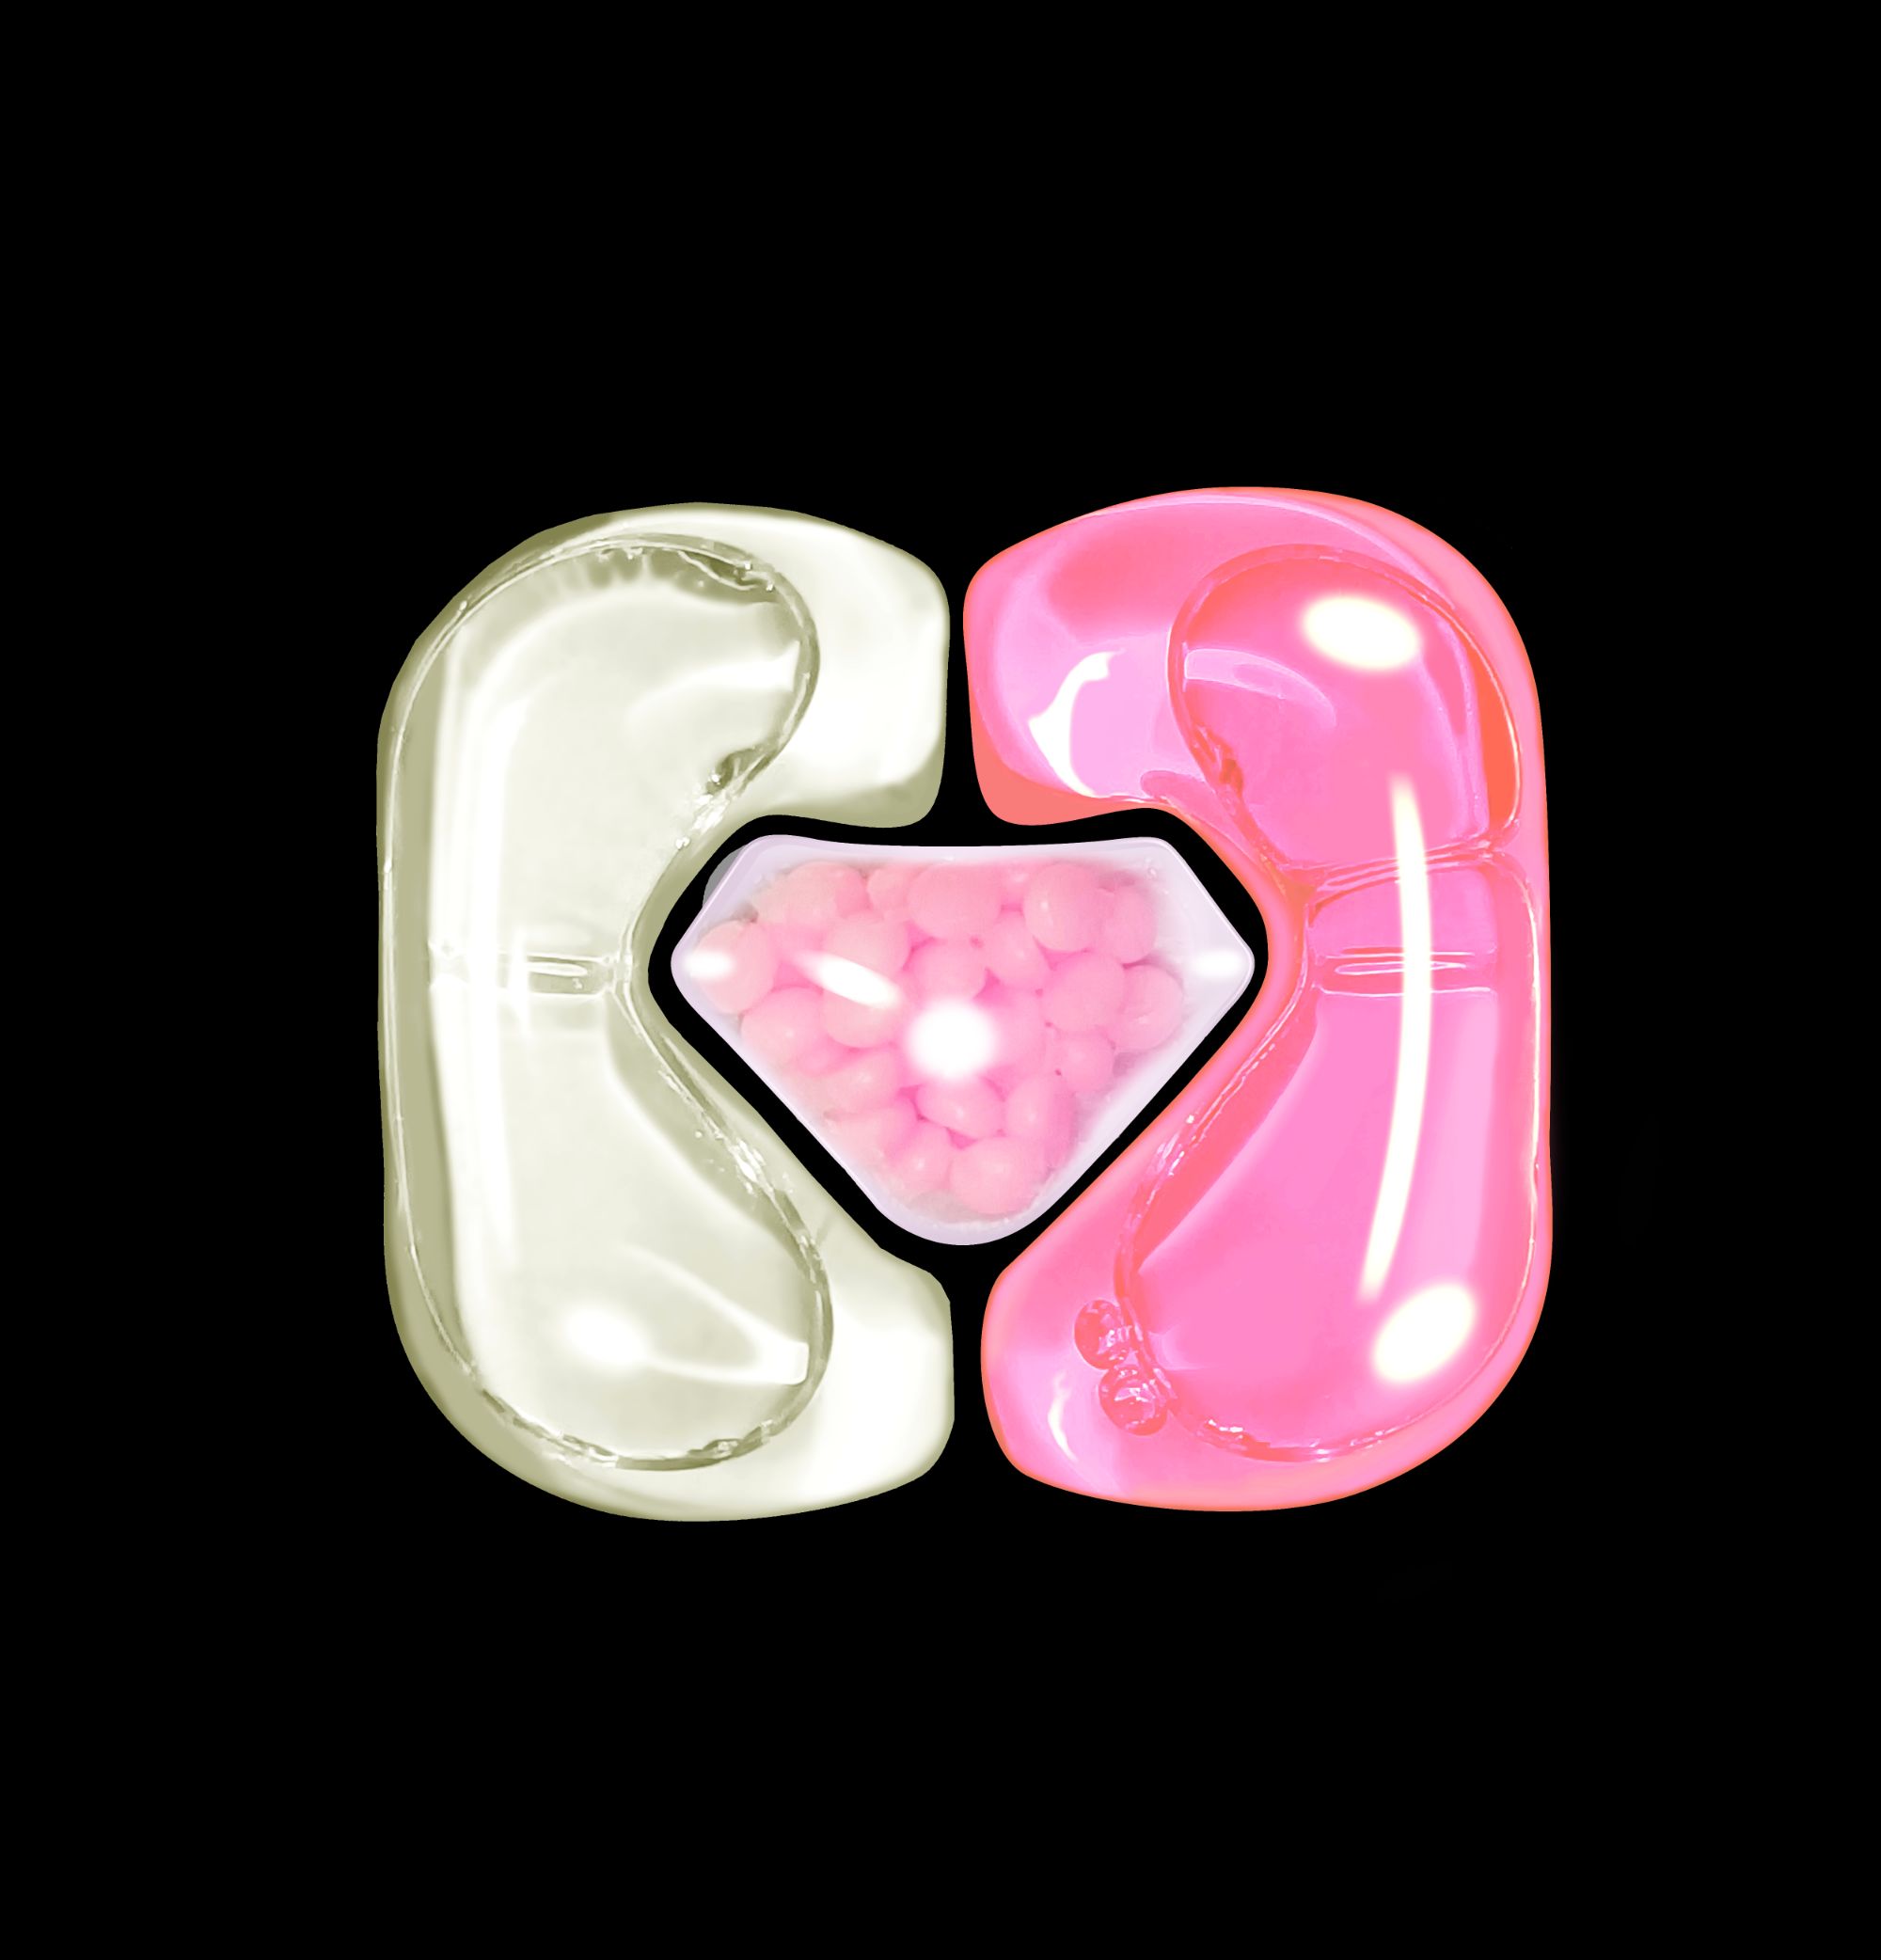
The first weak point is usually the film itself. On a bulk line, tiny shifts in humidity or sealing temperature get multiplied across thousands of pods, so the seams that looked fine in a sample run can start weeping detergent inside the box. Once that happens, the outer layer turns tacky and pods fuse together, which means the customer is already prying them apart before the machine door is even open.
Stacking and transport add another layer of trouble. The pods at the bottom of a pallet sit under constant pressure, and any slight brittleness in the film becomes a crack. Temperature swings inside a trailer or warehouse make it worse: the film expands and contracts, and the liquid core slowly finds the weakest corner.
Then there is the quiet chemical drift. Bulk pods often sit longer than retail packs, and without the extra barrier of a small carton or pouch, fragrance and enzymes lose their edge in humid air. What arrives at the wash is still technically a pod, but the cleaning performance has already slipped a notch.
What live production samples reveal that polished demo kits hide
Demo units are usually hand-finished to a standard that production rarely sees. Pull a live sample straight from the line and the small truths start showing up: minor sink marks near bosses, slightly uneven anodizing, a parting line that becomes obvious under side light, or fastener torque that shifts from unit to unit.
These samples also expose how materials behave when nobody has sorted or reworked them. A polished kit may have matched grain direction and selected connectors, but a production sample reveals the real spread of color, gloss, and fit. That variation is not automatically a defect; it is the actual boundary of the process, and it tells you what a customer will feel in their hands.
Assembly sequence and handling leave marks too. Fingerprints, light scuffs, or a label that sits slightly off on a live sample point to steps that need better fixturing or cleaner pickup points. Demo kits hide those because someone corrected them before they left the bench.
Comparing enzyme loads across detergent pod spec sheets without lab access
Checking a pod spec sheet for enzyme load usually means stepping around vague wording before you even get to the numbers. Some brands list individual enzymes by activity, such as protease at 1.2 U/g and amylase at 0.7 U/g, while others only print "enzymes" near the end of the ingredient block. If you are comparing sheets at home, first pull the same regional versions of each data sheet and safety sheet, because enzyme loads can shift by market. Then rewrite every entry as the amount delivered per pod, not per 100 grams of formula, since pod weights differ enough to distort a straight percentage comparison.
The next issue is that enzyme names are not interchangeable. A stain-fighting blend that lists only lipase may be less useful for protein-heavy laundry than a product listing separate subtilisin and mannanase even if the total enzyme weight looks lower. When percentages do appear, check whether they refer to the raw enzyme preparation or to active protein. A table showing "0.5% protease prep" next to "0.3% amylase active" cannot be read side by side without contacting the manufacturer. It is usually worth asking the company for the active protein basis or the activity units per pod, but you can get a rough ranking by comparing only the same enzyme types and the same basis.
Without lab access, dosage and wash conditions will also reveal part of the story. A sheet recommending one pod for a short cold cycle with visible protein stain removal implies a more robust or cold-active protease than a similar pod designed for long warm washes. You can also do a poor-man's test at home with identical stained swatches, same water hardness, same machine, and one pod per load, but treat that as a coarse screen rather than proof. The cleanest non-lab comparison comes from converting each sheet to enzyme activity per pod, using the same named enzyme, same basis, and same region, then letting the numbers sit side by side.
Setting rejection limits for warped pods and weak seals before signing
Rejection limits need to be locked down before anyone puts a signature on the line. For warped pods, the rule should cover more than just visible distortion. Measure rim flatness against the reference plate, and set a maximum gap that still allows the lid film to bond without pleats or channels. Anything that rocks when placed on a flat surface, or shows a flange deviation beyond the agreed gauge, goes straight to hold.
Weak seals are trickier because they can look acceptable under ambient light but fail later during transit or on the shelf. Run a burst test on samples from both the start and end of each sealing cycle, not just the middle. Set the lower limit high enough to survive temperature swings and rough handling, but not so high that the film tears at the edge. The exact number should come from package integrity data, not from a guess on the floor.
Once the limits are written down, pair them with a clear call on borderline units. If a pod is within 10% of the reject threshold or the seal shows uneven width beyond a set band, treat it as suspect. No signature should mean accepting those units; it should mean the line is cleared to run against those limits and that out-of-spec material is removed without needing a debate at the end of the shift.
The real cost per usable detergent pod after breakage and returns
Breakage doesn't simply mean a few lost pods in the bottom of the box. Every cracked or punctured pod leaks detergent into the packaging, coating the remaining pods and forcing you to rinse or discard them before they ever reach the washing machine. That waste compounds quickly, especially when a single broken pod can ruin the surface of three or four perfectly good ones. Returns add another layer: customers open a container, find a sticky mess, and send it back. The retailer refunds the purchase, but the manufacturer absorbs the freight, inspection, and disposal costs, none of which are recoverable.
To calculate the true per-unit expense, you need to separate usable pods from the total shipped. Start with the billed quantity, subtract the pods destroyed directly by breakage, then subtract the share of pods inside returned units that can't be salvaged. Divide your total landed cost—material, production, packaging, freight, and return processing—by that smaller usable number. A box that appears to cost 18 cents per pod at retail might end up costing 24 or 26 cents per pod once hidden losses are counted.
The gap between nominal cost and real cost widens further when breakage rates fluctuate by season or shipping route. Hot warehouses soften the pod film, long-haul truck vibrations crack seams, and e-commerce parcels get dropped on doorsteps. Tracking breakage and return data by batch, not just by month, reveals which packaging designs or shipping methods are quietly draining margin. Fixing those patterns usually beats negotiating a fraction of a cent off the raw film price, because the savings flow straight to the number of pods that actually make it into a drum.
Packaging specs that matter in humid storage and long shipping routes
Humidity doesn't announce itself until it's already inside the carton. A pallet that left the warehouse feeling dry can arrive at port with condensation trapped between film layers, wicking through corrugated corners, or settling into unlined caps. For routes that cross multiple climate zones, the real spec to watch isn't just the moisture barrier rating on a data sheet—it's how the package behaves after 40 days of temperature swings. Foil laminates and desiccant packs help, but only if the seal geometry and vent placement work together. A well-designed vent can release pressure without letting ambient moisture sneak back in during the cooler night leg.
Long shipping routes expose another quiet failure point: stacked compression under high humidity. A box that holds its shape at 50% RH may soften noticeably at 75% RH, especially if the flute structure absorbs moisture from open edges. Specifying edge crush values without conditioning the samples to expected transit humidity gives a false sense of safety. Instead, look for board combinations that retain at least 80% of their dry strength after 24 hours at 85% RH. That number says more about real-world survival than any single burst test run in ideal conditions.
Sealing specs need the same kind of realism. Tape adhesion drops when the carton surface carries a thin moisture film, and staples or stitching can become corrosion points if the metal isn't coated for marine exposure. For humid storage and extended ocean legs, the practical checklist should include: coated staples or no metal fasteners, full-height tape patterns with moisture-resistant adhesive, and liner choices that don't delaminate when the outer ply absorbs water. These details matter less in a short domestic lane, but on a six-week route through the tropics they're the difference between a product arriving intact and a crate arriving as pulp.
FAQ
Ask for a full ingredient sheet and pay attention to the surfactant level, not just the fragrance story. The best suppliers will name the specific enzymes and their expected activity. Vague answers about a proprietary blend are fine up to a point, but the core cleaning ingredients should be transparent.
Request a sample pack and leave it in a warm, humid area for a couple of weeks. If the film starts to soften, stick together, or leak, that's a sign of weak PVA or poor sealing. Also ask for the recommended storage temperature range and compare it with your actual shelf conditions.
Not always. Some lower prices come from thinner packaging, smaller pod size, or fewer enzymes per pod. Compare cost per wash, not just cost per unit. Ask the supplier how many grams of surfactant and enzyme go into each pod; a cheap pod that needs two per load is often more expensive in the long run.
Don't let a wholesaler push you into a container just to get a lower unit price. Start with the smallest order that still gives you a workable margin, then test sell-through. Many suppliers will allow a mixed pallet or half-pallet for the first order if you ask directly.
Yes, and you should be wary of any wholesaler that refuses. Ask for samples from the actual production line, not a pre-made marketing kit. Run them through normal washes at different temperatures and with hard water if that matches your customer base. Pay attention to residue after the rinse cycle.
Check the film thickness, the seal strength, and whether the container has a child-resistant closure. If the pods arrive in bags, make sure they are double-sealed and not prone to tearing at the seams. Also ask if the packaging is moisture-resistant enough for your storage area.
Ask the supplier for performance data in hard water, not just soft water demos. A good formula will include chelating agents or builders that handle mineral buildup. If they can't provide that data, run your own test with a high-mineral water source and compare stain removal and residue.
Start with one reliable supplier so you learn how the product moves and how customers respond. Once you have consistent demand, you can test a second supplier with a smaller order to compare fill rates, shipping times, and complaint levels. Avoid switching too quickly, because continuity helps build trust with repeat buyers.
Conclusion
Buying detergent pods in bulk rarely goes wrong at the quote stage; it goes wrong in the gap between a polished sample and what actually lands on the pallet. Ask for live production pulls, not handpicked demo kits, because those clean, uniform pods from a sales meeting often hide the real story: slightly underfilled cavities, uneven film tension, or a seal that looks fine until humidity does its work. Pay attention to enzyme loads on spec sheets, but do not treat them as equal. Two suppliers can list protease and amylase on paper while using very different activity levels, which changes how well a pod handles grease or stains in cold water. If you cannot run lab tests, ask for guaranteed minimum enzyme activity per pod and batch-level documentation.
Before signing, set measurable rejection limits for warped pods, leaking film, and weak seals, and make sure those numbers appear in the purchase agreement rather than in a side conversation. Then calculate the true cost per usable pod: breakage during transit, customer returns, and pods that dissolve into a sticky mess are not minor annoyances; they eat directly into margin. Packaging deserves the same scrutiny as the formula itself, especially if cartons will sit in humid warehouses or travel long routes. Moisture-barrier films, reinforced corners, and pallet configuration all determine whether pods arrive intact. A slightly higher unit price can be cheaper overall when fewer pods are wasted before the first wash.
Contact Us
Contact Person: Zhao Yanlong
Email: [email protected]
Tel/WhatsApp: 8615832007309
Website: https://www.gzlanjieya.com