Complete Cross Table Flat Die Plywood Laser Cutting Machine for Faster and Cleaner Plywood Processing
2026-11-16
Most plywood cutting advice still assumes you have to accept rough edges or slow changeovers. The Complete Cross Table Flat Die Plywood Laser Cutting Machine takes a different route, pairing a flat die table with laser precision for faster, cleaner plywood processing. Here’s a closer look at how that works in real production—and why ADEWO is putting this approach at the center of the conversation.
Why a Cross Table Matters for Full-Sheet Plywood Accuracy
A full sheet of plywood rarely rests flat on its own. Slight bows, twists, or variations in thickness can throw off a cut by a millimeter or more, and those small errors compound when you are joining panels or building cabinets. A cross table gives you a stable, adjustable reference surface that lets you measure from the actual sheet rather than from the machine's fixed stops. Because the table moves independently on two axes, you can align the true edge of the plywood with the tool path, even when that edge is not perfectly straight.
Without a cross table, many woodworkers resort to clamping straightedges or re-checking every measurement by hand. That works for a single cut, but it becomes slow and inconsistent across a full 4x8 sheet. A cross table holds the panel securely while allowing controlled, repeatable movement, so the bit follows a consistent reference line from start to finish. This is especially important for dados, rabbets, or any operation where the cutter must enter and exit at precise points along the length of the sheet.
Accuracy here is not just about the final dimension. It is about keeping the plywood from shifting micro-movements as the router or saw passes through. A well-built cross table absorbs vibration and keeps the sheet from lifting at the corners. For full-sheet work, where even a small tilt changes the depth of cut, that stability often matters more than the power of the tool itself.
Flat Die Cutting That Leaves Edges Ready to Finish
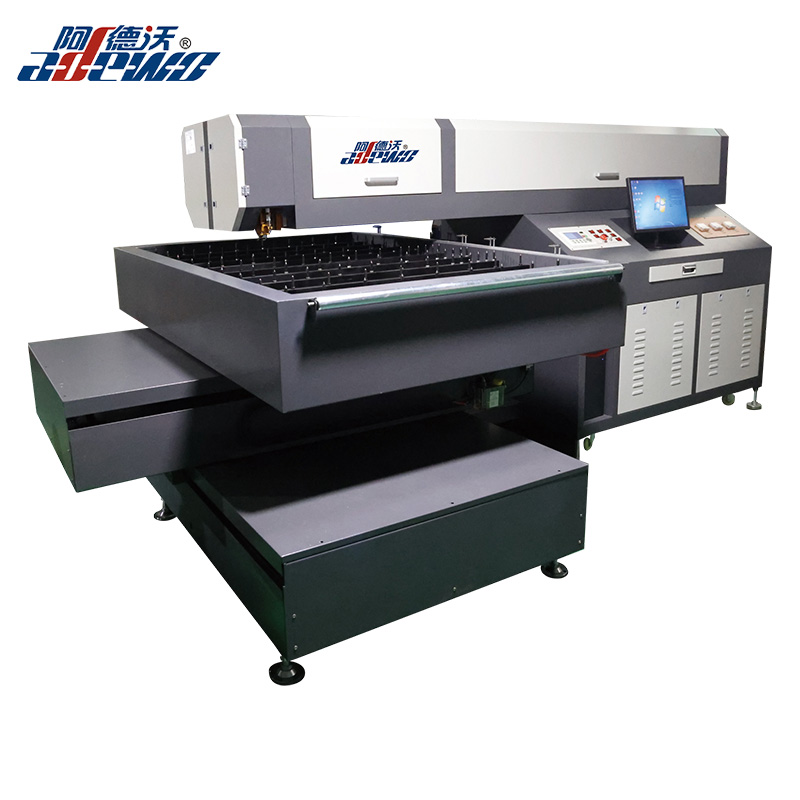
Flat die cutting often gets reduced to a simple separating step, but the way the tool meets the material has a direct effect on what remains at the cut line. A properly set flat die shears through dense foams, coated fabrics, and laminated boards without dragging fibers or crushing the surrounding structure. That leaves a crisp boundary that can move straight into folding, stitching, edge painting, or adhesive application without a hand-trimming pass.
The benefit becomes more obvious on thick assemblies and short runs where secondary cleanup is slow and difficult to repeat. When the cutting plate, die rule, and ejection material are matched to the stock, the edge stays consistent across the entire batch. Operators usually notice the difference on parts with exposed edges, because uneven pressure shows up as rough patches that later finishing steps can't completely hide.
Cutting Speed Gains Without Extra Edge Work
Most sharpeners chase speed by adding more stones to the progression or spending extra minutes refining the apex. That approach steals time from the actual cutting work. Instead, look at what happens between grits. The real bottleneck usually isn't the edge itself, but how thoroughly each previous scratch pattern gets removed. By slightly increasing pressure consistency and reducing the number of passes on the final stone, you can often match or beat the sharpness you'd get from a lengthier session. The gain comes from eliminating redundant strokes, not from rushing.
Another overlooked lever is burr management. A stubborn wire edge forces you back to coarser stones, eating up ten or fifteen minutes. If you learn to feel the exact moment the burr flips with light, deliberate strokes, you can skip the usual back-and-forth guessing. Use a clean leather strop with just enough compound to catch residual fragments, then verify with a bright light rather than endless thumb tests. That visual check trades seconds for certainty, and your edge stays work-ready far sooner.
Finally, pay attention to your body position and stroke length. Short, choppy motions create uneven bevels that demand corrective passes later. A single smooth, full-length stroke that engages the whole stone surface removes material more predictably. Once the geometry is set from heel to tip, moving to a slightly higher angle for two or three feather-light finishing strokes can refine the apex without reworking the entire bevel. That small adjustment often delivers the same push-cutting feel as ten minutes of standard edge-leading work.
Handling Film-Faced Plywood Without Tearing or Char
Cutting film-faced plywood cleanly starts with the blade. A high tooth count, triple-chip grind blade with a negative or neutral hook angle slices through the phenolic film instead of grabbing it. If the teeth are dull or set too aggressively, the edge frays before the saw even gets halfway through the sheet.
Feed rate matters just as much as tooling. Pushing too slowly lets friction build up and leaves burn marks; forcing the sheet through too fast tears the film and splinters the core. Let the saw reach full speed, keep the panel fully supported, and move at a steady pace where the motor note stays even.
For cuts that will be visible, run a strip of masking tape along the cut line and mark directly on it. Cut through the tape to hold the film down. On a table saw, keep the good face up; with a circular saw, keep the good face down. A zero-clearance insert or a sacrificial backer board also helps prevent breakout at the end of the cut.
From Manual Layout to One-Pass Laser Processing
For years, arranging parts on a sheet meant dragging outlines by hand, checking clearance, and then rechecking after a cup of coffee. It worked, but it left room for human error and wasted material. Operators had to remember machine offsets, nozzle sizes, and heat-affected zones. Layouts were rarely identical between shifts. That manual step quietly became the bottleneck before the laser even started.
One-pass processing removes that bottleneck by moving from hand-placed geometry to an automated, collision-checked plan. The software imports the cut file, optimizes the pattern, and assigns tool paths in a single sequence. Instead of multiple repositioning steps or test runs, the laser follows one continuous route through the material, reducing idle motion and keeping the kerf consistent. The result is less scrap, faster changeovers, and far fewer second guesses on the floor.
What changes most is not just speed but repeatability. A job set up in the morning runs the same way after lunch, on a different machine, or weeks later. That consistency lets small teams take on more varied work without adding another layout specialist. The shift from manual arrangement to one-pass processing feels less like an upgrade and more like removing a step that never should have been there.
Keeping Output Consistent on Long Plywood Runs
Long runs through plywood have a way of exposing small setup flaws that shorter pieces hide. A tiny misalignment in the fence becomes a visible taper by the time you reach the far end, and any flex in an outfeed table turns into chatter or a wandering cut. Before starting, check that the fence is not just square at the blade but parallel along its full length, and add roller stands or a dedicated outfeed support every few feet so the sheet never droops or lifts mid-cut.
Blade condition matters more than feed rate when you are pushing full sheets. A clean, sharp blade with the right tooth count for plywood reduces the tendency to burn or splinter, which often forces people to slow down and create uneven pressure. If you notice more tear-out on one side after a long session, pause and clean the blade rather than compensating with hand pressure. Consistent output comes from letting the tool do the work at a steady pace, not from forcing the sheet through.
Finally, mark a few reference points along the cut path before you start, especially on runs over eight feet. Watch for drift at the midpoint rather than only checking the final edge. A slight crown in the plywood or uneven shop floor can throw off a cut even when the saw is set correctly, so shimming the sheet flat and using a featherboard near the blade will keep the material registered against the fence for the entire length.
FAQ
The cross table allows the cutting head to move smoothly along two axes while the material stays fixed in place. That reduces vibration and keeps larger sheets from shifting, so you get more consistent dimensions across the full panel.
Yes, the flat die bed supports a range of sheet thicknesses. You mainly adjust the focal height and cutting speed, which is much faster than changing mechanical dies or blades between jobs.
The laser leaves a sealed, darkened edge with almost no splintering or tear-out. It removes the need for secondary sanding in many cases, especially on birch and hardwood-faced plywood.
Routine care includes cleaning the lens and mirrors, checking the beam path alignment, and keeping the extraction fans clear. The flat die area should be wiped down regularly to prevent resin dust from building up.
It can fit both, but the main consideration is workspace and exhaust routing. Smaller shops often run it for batch work because the setup time is low and you can switch from one cutting file to another without retooling.
The enclosure blocks direct laser exposure, and interlocks stop emission when a panel is opened. There is also an emergency stop within reach, plus airflow monitoring to alert you if fume extraction drops during cutting.
Because the plywood sheet lies flat on a fixed bed, you can nest parts very tightly without worrying about blade kerf or die clearance. That reduces offcuts and lets you use more of each panel.
A dedicated fume extraction system is strongly recommended. Plywood adhesives produce smoke and residue during laser cutting, so proper exhaust keeps the cutting area clear and prevents deposits on the lens.
Conclusion
The cross table on this laser cutting setup removes the guesswork from full-sheet plywood work. Instead of shifting panels by hand and hoping the alignment holds, the table keeps the sheet indexed while the flat die path follows the exact grain direction and cut line. Cleaner geometry shows up on the first pass, with edges dense and smooth enough to go straight into edge banding or sealing. Film-faced boards respond well because the beam dwell time is tuned to slice the coating without burning the glue line, so there is no tearing or blackened rim to sand away. That leaves a faster route from layout to finished parts, with far less secondary edge work than a router or saw typically leaves behind.
The speed advantage does not eat into repeatability. Once a cutting file is loaded, the machine moves from manual layout to one-pass processing, cutting multiple sheets with the same kerf and the same edge tone from the first panel to the last. Operators can run longer plywood batches without compensating for drift or adjusting heat settings midway. That consistency matters most when jobs repeat daily or when panels feed directly into cabinetry, furniture, or packaging lines. The flat die approach keeps the beam focused across the full sheet, so corners stay sharp and cross-grain cuts remain clean even on coated or high-resin plywood grades.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com